Blog
7 Best Aluminium Tri Fold Blind Rivets for Composites
Composite structures are expanding across transportation, marine, construction, and renewable-energy applications. Industry reports from MarketsandMarkets and Grand View Research consistently forecast strong growth in global composites demand through 2030. That growth increases the need for fastening systems that protect delicate laminates during installation and service.
This guide examines seven Aluminium Tri-Fold Blind Rivets for Composite Materials, focusing on grip range, head design, mandrel retention, corrosion resistance, and installation consistency. Tri-fold rivets spread their legs behind the panel, creating a broad bearing area. That detail matters when thin fiberglass, carbon-fiber, or sandwich panels could crush under concentrated pressure.
Dr. Stephen W. Tsai, a respected composites researcher, has emphasized a practical design principle: “The joint is part of the structure, not an afterthought.” His message fits blind-rivet selection precisely. A rivet may look suitable in a catalog, yet fail to match the laminate thickness or load path.
Real workshop experience also reveals small differences. A washer may prevent surface pull-through. A sealed body may reduce moisture entry. Correct nosepiece alignment can improve repeatability.
No single rivet suits every composite assembly. That is the uncomfortable part. Material compatibility, hole quality, access limitations, and vibration exposure can change the result. ASTM and SAE fastening guidance should support product data, not replace it.
The following comparison therefore balances published specifications with practical installation concerns. It also recognizes a common weakness: many product listings provide impressive strength figures without explaining test conditions. Careful readers should question those numbers before choosing a fastener.
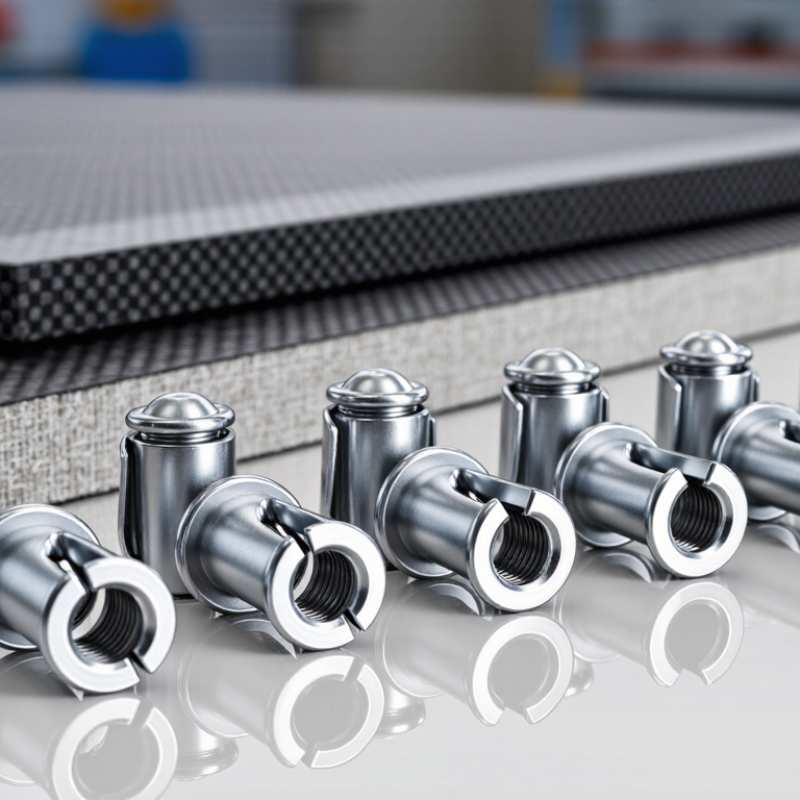
Aluminium Tri-Fold Rivets for Composites: A Technical Ranking of 7 Options
Aluminium Tri-Fold Rivets for Composites: A Technical Ranking of 7 Options
A practical ranking should consider pull-through resistance, galvanic risk, clamp load, and hole quality. MarketsandMarkets valued the global composites market at approximately USD 126 billion in 2023. That scale increases demand for reliable, lightweight fastening. Load spreading matters. My technical ranking is: 1) large-flange aluminium body with aluminium mandrel; 2) sealed large-flange version for moisture exposure; 3) low-profile tri-fold rivet for thin skins; 4) countersunk tri-fold rivet for flush surfaces; 5) standard-flange aluminium rivet for non-structural panels; 6) aluminium body with stainless-steel mandrel; 7) small-flange rivet for dense laminate sections.
The first two options usually distribute force across a wider surface. They suit sandwich panels, fairings, and lightweight enclosures. A sealed body can reduce water entry, but it may complicate inspection. Low-profile designs improve clearance, although their smaller bearing area deserves testing. Countersunk versions look clean. They can weaken thin composite skins if the recess is too deep. ASTM D5961 testing helps evaluate bearing response in composite laminates, while ISO 14589 supports blind-rivet mechanical verification.
Material pairing remains critical. Aluminium against carbon-fibre composites can create galvanic corrosion, especially near saltwater or trapped moisture. A protective coating, barrier washer, or compatible isolating layer may be necessary. The seventh option ranks lowest, not because it always fails, but because narrow flanges can concentrate stress. This ranking is not universal. Real results change with laminate thickness, core density, grip range, and installation force. A neat joint can still be a weak joint. I would validate every selection with pull-through and environmental testing before production use.
| Rank | Rivet Configuration | Nominal Diameter | Typical Grip Range | Recommended Hole Diameter | Head Style | Typical Body Material | Mandrel Choice | Composite Suitability | Best Application | Technical Assessment | |
|---|---|---|---|---|---|---|---|---|---|---|---|
| 1 | Large-Head All-Aluminium Tri-Fold Rivet | 4.8 mm | 3.0–6.0 mm | 4.9–5.0 mm | Large flange, dome head | Aluminium alloy body | Aluminium mandrel preferred | Excellent | Thin glass-fibre or carbon-fibre panels where surface load distribution is important | Large bearing area helps reduce local crushing and pull-through. The all-aluminium construction also limits galvanic risk when used with aluminium fixtures. | 9.3/10 |
| 2 | Medium-Grip All-Aluminium Tri-Fold Rivet | 4.8 mm | 6.0–10.0 mm | 4.9–5.0 mm | Large flange, dome head | Aluminium alloy body | Aluminium mandrel preferred | Excellent | Sandwich panels and composite-to-composite joints with moderate combined thickness | Provides a broad rear-side bearing pattern while accommodating thicker laminates or core-backed panels. Correct grip selection is essential for full folding. | 9.1/10 |
| 3 | Short-Grip Aluminium Tri-Fold Rivet with Sealing Washer | 4.8 mm | 1.5–4.0 mm | 4.9–5.0 mm | Large flange, dome head | Aluminium alloy body | Aluminium mandrel or corrosion-isolated steel mandrel | Very good | Thin exterior skins, covers, fairings and lightly loaded enclosure panels | The sealing washer improves resistance to water ingress at the joint. It is best suited to thin material and should not be used to compensate for an incorrect grip range. | 8.8/10 |
| 4 | High-Strength Aluminium Tri-Fold Rivet | 6.4 mm | 4.0–8.0 mm | 6.6–6.7 mm | Large flange, dome head | Work-hardened aluminium alloy body | Stainless-steel mandrel with electrical isolation | Very good | Higher-load composite brackets, thicker laminates and structural covers | The larger diameter can provide greater joint capacity, but it also requires more edge distance and a carefully controlled hole to avoid delamination. | 8.6/10 |
| 5 | Long-Grip Aluminium Tri-Fold Rivet | 6.4 mm | 8.0–12.0 mm | 6.6–6.7 mm | Large flange, dome head | Aluminium alloy body | Corrosion-isolated steel mandrel | Good | Thick sandwich constructions, bonded inserts and multi-layer composite stacks | Useful when the total stack thickness is substantial. Excessive grip can prevent complete folding and may leave an uneven rear-side joint. | 8.2/10 |
| 6 | Countersunk Aluminium Tri-Fold Rivet | 4.8 mm | 3.0–6.0 mm | 4.9–5.0 mm | Countersunk head | Aluminium alloy body | Aluminium mandrel preferred | Good | Flush aerodynamic or low-profile composite surfaces | Offers a flush external finish, but countersinking removes laminate material and can reduce local strength. Use only with adequate laminate thickness and edge distance. | 7.8/10 |
| 7 | Aluminium Tri-Fold Rivet with Stainless Mandrel | 4.8 mm | 3.0–6.0 mm | 4.9–5.0 mm | Large flange, dome head | Aluminium alloy body | Stainless-steel mandrel | Good with isolation | Outdoor composite assemblies exposed to vibration, moisture or elevated installation loads | The stainless mandrel can improve mandrel retention and durability, but aluminium-to-stainless contact requires sealant, coating or another suitable galvanic-isolation method. | 7.6/10 |
Technical note: Dimensions and grip ranges shown are common configuration ranges for aluminium tri-fold blind rivets, not a substitute for a manufacturer’s certified data sheet. For composite laminates, use a sharp drill, support the exit surface, maintain adequate edge distance, and verify joint performance with representative pull-through and shear testing.